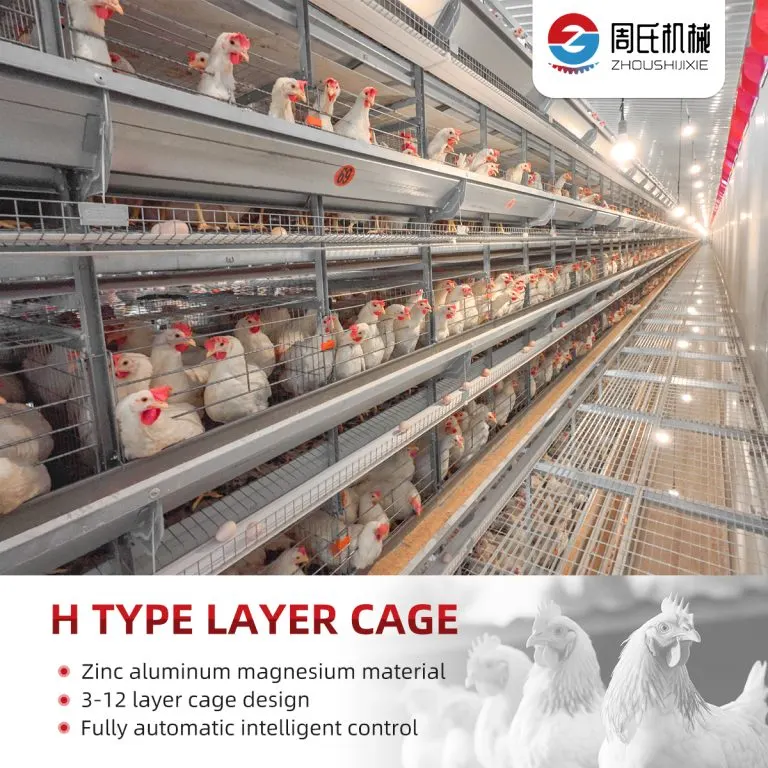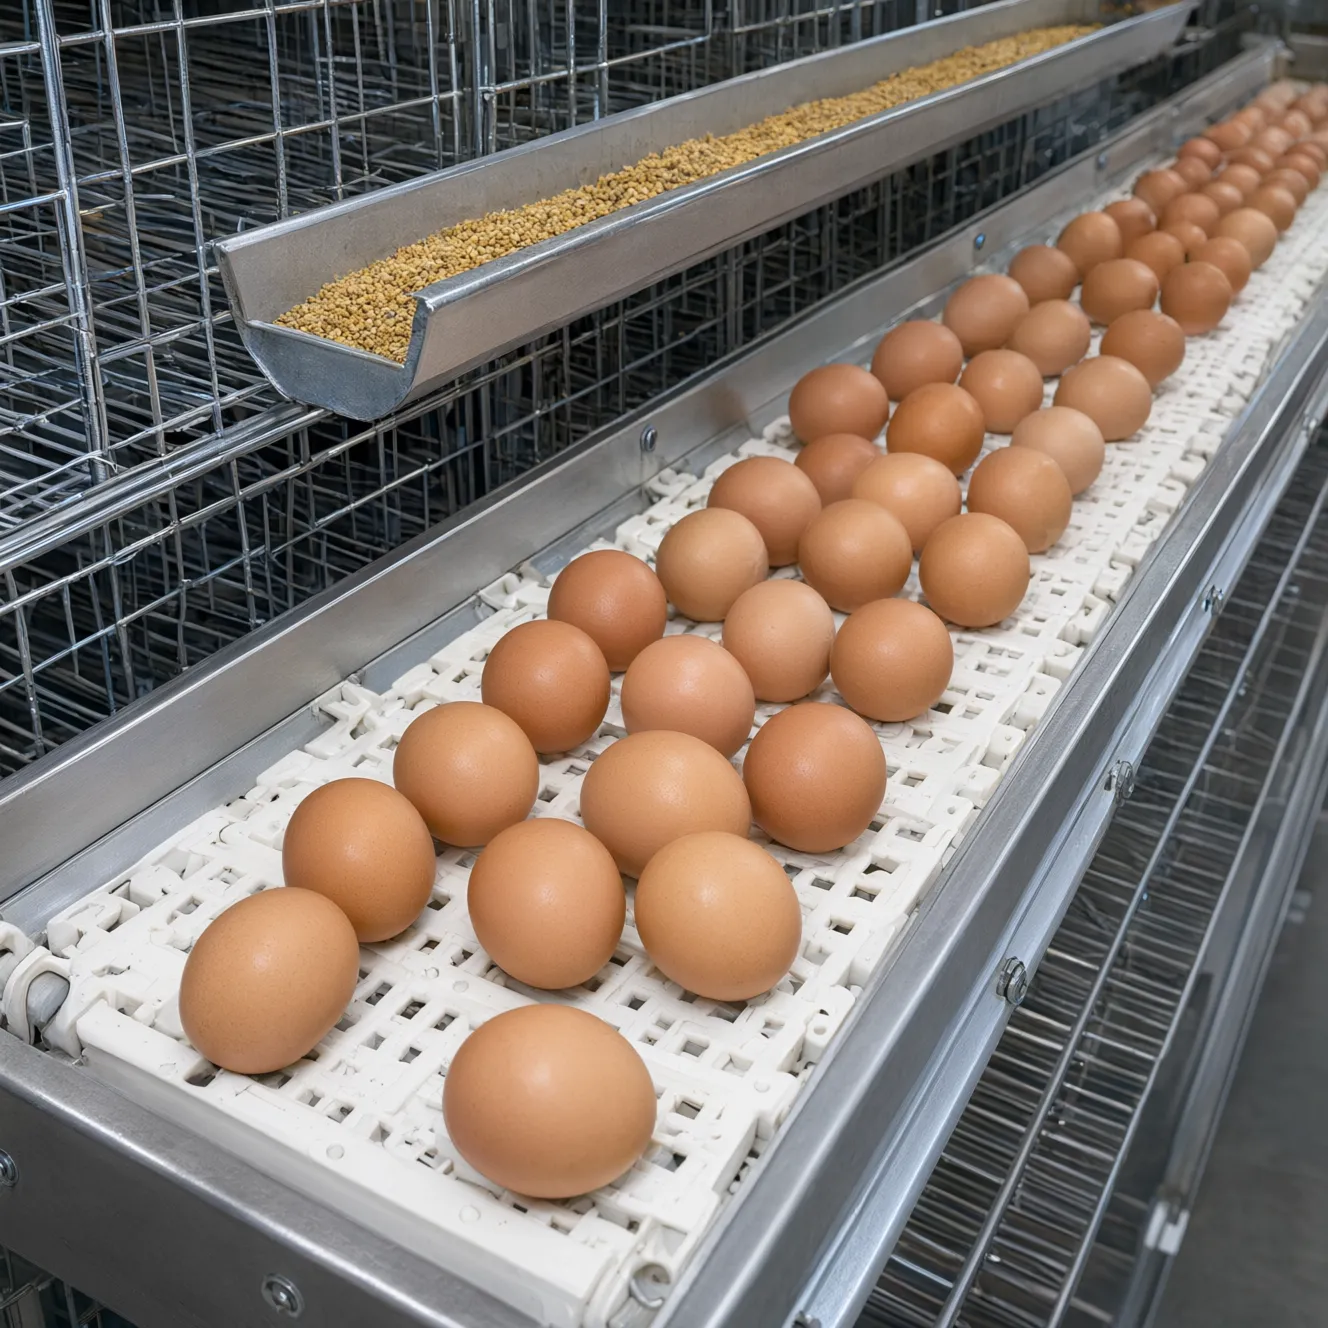
Elevator-type automatic egg collection up to 65,000 eggs per hour, nest-box systems for floor and welfare houses, and central egg handling to the grading room.
Egg Collection System projects fail on three things: material spec, system integration and after-sale parts. Our answer to all three is vertical integration — frames, belts, drives and controllers leave one plant in Cangzhou, share one spare-parts catalog, and get drawn into one layout before you pay a deposit.
The difference between collecting eggs and not losing eggs: controlled speed, soft-egg filterin
Floor eggs are graded-out eggs. Give hens the dark, soft nest they want and take the eggs away
Specification sheets are commodity; integration is not. A egg collection system only performs when its row geometry matches the house, its drive loads match the voltage at the site, and its consumables are in stock when a belt fails on a Saturday in peak season. These are supplier-selection criteria, not product features — and they are the reason buyers in 60+ countries standardize on one manufacturer per farm rather than one product per purchase.
Our process is fixed: you send flock target and house dimensions; we return layout drawings, a bill of materials and FOB pricing within about 24 hours; production, galvanizing and packing follow with video checkpoints; and the lifelong-consultant line stays open after the containers are gone — because a farm that succeeds in year two reorders in year three.
Send us your flock size, house dimensions and budget — our engineers reply with cage layout drawings, equipment list and FOB price, usually within 24 hours.